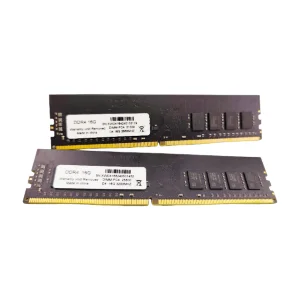
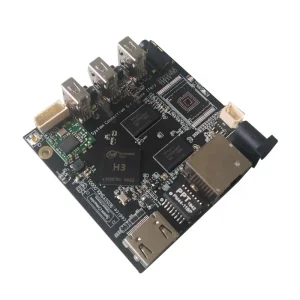
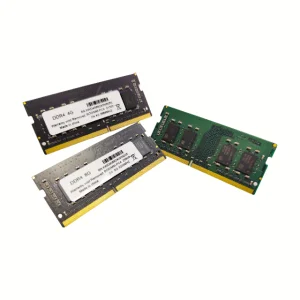
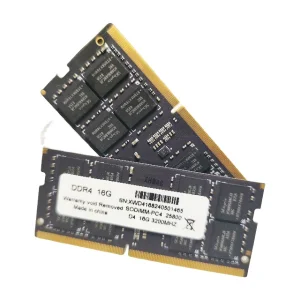
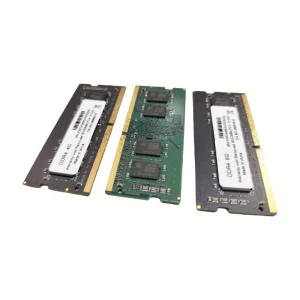
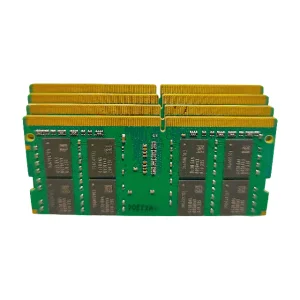
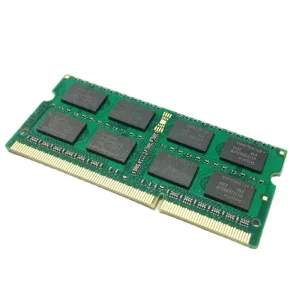
Advanced SMT-integrated controller boards, high-speed RAM buffers, and embedded system processing units engineered to drive high-intensity UVC sanitation platforms in biomedical and clinical operations.
Geneva, globally recognized as a center for international diplomacy, biotechnology research, and precision engineering, demands the highest standards of sterilization and hygiene control. The canton’s booming life science cluster (anchored by centers like Campus Biotech) and its world-class medical institutions require cutting-edge solutions to prevent contamination. Historically, chemical disinfectants and mercury-based UV lamps dominated these spaces. Today, under the pressure of the Minamata Convention on Mercury and strict Swiss environmental regulations, Geneva’s industrial stakeholders are accelerating the migration to mercury-free, high-efficiency UVC LED modules.
Beyond clinical cleanrooms, Geneva’s municipal projects—especially those managing Lac Léman (Lake Geneva) water quality and complex building automation networks (like the *GeniLac* hydrothermal system)—face strict regulatory guidelines. Ensuring biological safety without introducing toxic byproducts is paramount. This creates a specific, high-intent local demand for customized, solid-state UVC disinfection systems capable of operating under precise flow rates, high optical output requirements, and integration with local IoT infrastructure.
While 254nm was the standard for low-pressure mercury lamps, solid-state AlGaN (Aluminum Gallium Nitride) semiconductor technology permits precise targeting. We customize our modules to emit peak germicidal wavelengths at 265nm - 275nm, which aligns perfectly with the DNA/RNA absorption peak of pathogens like *Legionella pneumophila* and *Pseudomonas aeruginosa*. Additionally, our research into far-UVC (222nm) offers paths for safe, occupied-room disinfection.
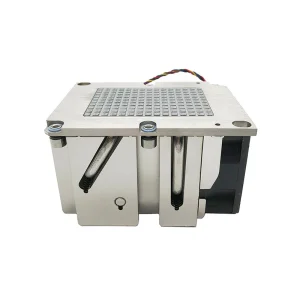
UVC LEDs exhibit a low wall-plug efficiency (WPE) compared to visible LEDs, converting up to 95% of electrical energy into heat. Our design uses high-conductivity copper-core PCBs (MCPCB), thermoelectric coolers (TEC), and customized aluminum heatsinks designed to keep junction temperatures (Tj) below 65°C. This strict thermal budgeting ensures an operating lifetime (L70) exceeding 15,000 hours.
We utilize advanced optical simulation tools to design customized quartz lenses with beam angles varying from narrow 30° spot profiles for high-intensity surface exposure to wide 120° flooding patterns. This prevents optical loss, ensuring that the target surface or liquid receives the specified target dose (measured in mJ/cm²) under varying dynamic flow rates.
Our integrated UVC LED solutions bridge the gap between basic component manufacturing and mission-critical European industrial system requirements.
Water safety in public networks, luxury spas, and laboratory chillers requires constant monitoring. Our water-disinfection UVC reactors are designed with flow-through chambers optimized by CFD (Computational Fluid Dynamics).
By integrating digital sensors, these systems communicate with Swiss building management systems (BMS) via Modbus or BACnet protocol. Real-time irradiance tracking adjusts UVC LED output power based on water turbidity, optimizing energy consumption while guaranteeing log-4 pathogen reduction.
Get Municipal Solution SpecsExporting advanced technical hardware to Geneva requires adherence to a multi-tiered regulatory framework. At the national level, the Swiss Federal Office of Public Health (FOPH/BAG) supervises biocide declarations. We ensure our UVC modules comply with all chemical risk ordinances (ChemRRV) and electrical standards.
Furthermore, as European integrations dictate, all our products possess full CE mark validation, including compliance with:
Through our Swiss representative network, we offer certified functional testing reports, optical safety labels, and local technical support in French, German, and English, smoothing the regulatory pathway for OEM integrators.
In our ultra-modern manufacturing site, we combine precision SMT lines, automated optical inspection (AOI), and continuous testing routines to deliver zero-defect optoelectronic components. Our manufacturing ecosystem integrates high-speed SMT mounting, wire bonding, thermal adhesive deposition, and final validation.
Because UVC LED efficiency relies heavily on high-integrity packaging (such as hermetic sealing with quartz covers), our class 10,000 cleanrooms are monitored for particle pollution and humidity levels. By co-developing the driver electronics, thermal solutions (including high-power heat pipes), and the LED modules under one roof, we eliminate intermediate supply chain delays and reduce manufacturing tolerance stackups.
This vertical integration allows us to keep production costs down while maintaining strict quality control. Our scale ensures that we can quickly pivot from high-volume batch runs for mass-consumer disinfection appliances to low-volume, highly complex custom designs for Swiss scientific research labs.
Founded in 2017, Memvora Electronics Technology Co., Ltd. is a professional manufacturer specializing in high-performance DDR5 memory modules, dedicated to delivering reliable memory solutions for consumer, industrial, enterprise, and embedded applications worldwide. With a modern manufacturing facility covering 386㎡, we combine advanced production equipment, strict quality management, and experienced engineering expertise to provide stable, high-speed memory products for global OEM and ODM partners.
Since entering the international market, Memvora has accumulated 7 years of export experience, serving customers across North America, Europe, Southeast Asia, the Middle East, and South America. Our annual export revenue exceeds US$18.6 million, supported by a strong global supply chain and long-term partnerships with more than 1,280 component suppliers and business partners.
With 14 years of industry experience, our team continuously invests in technology innovation and product development. Our R&D department consists of 126 professional engineers who focus on developing next-generation DDR5 memory solutions with higher speed, lower latency, and enhanced reliability. Last year alone, we successfully launched 86 new memory products to meet the evolving needs of gaming, AI computing, industrial automation, and enterprise servers.
Quality is the foundation of everything we do. Every product undergoes 100% functional testing, burn-in testing, compatibility testing, signal integrity testing, and aging tests before shipment. Our dedicated quality control team of 42 inspectors ensures every memory module meets rigorous international quality standards and delivers long-term stable performance.
Memvora provides flexible OEM, ODM, private label, custom capacity, PCB color, heat spreader design, firmware optimization, and packaging customization services to meet different market requirements. Backed by a responsive engineering team and efficient production management, we help customers shorten development cycles and accelerate product launches.
Today, Memvora serves a diverse customer base including memory brands, computer manufacturers, industrial equipment suppliers, system integrators, distributors, wholesalers, and e-commerce retailers. Through continuous innovation, reliable quality, and customer-focused service, we are committed to becoming a trusted global partner for advanced DDR5 memory manufacturing and customized DRAM solutions.
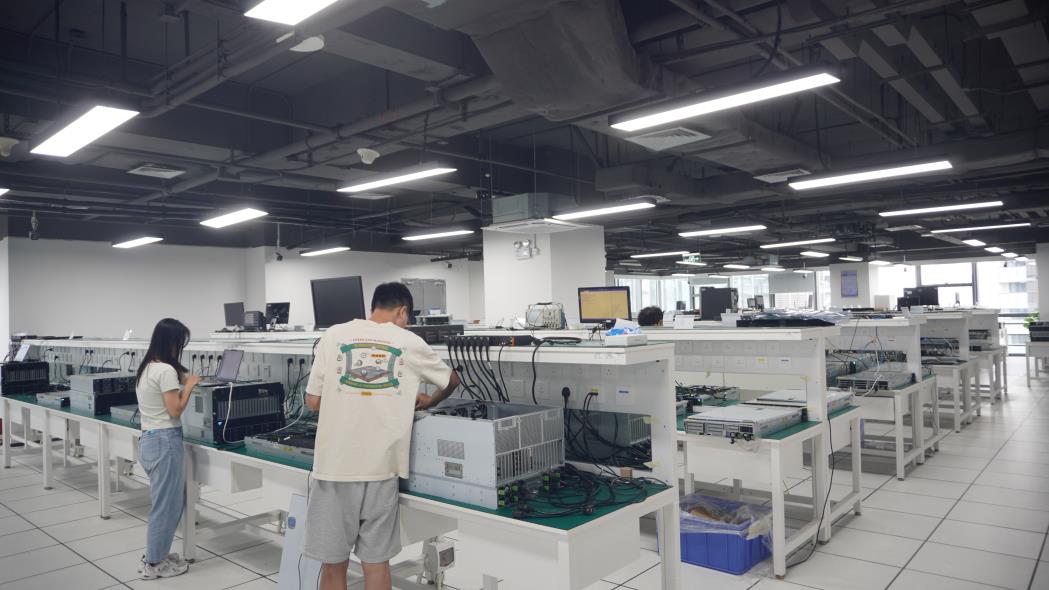
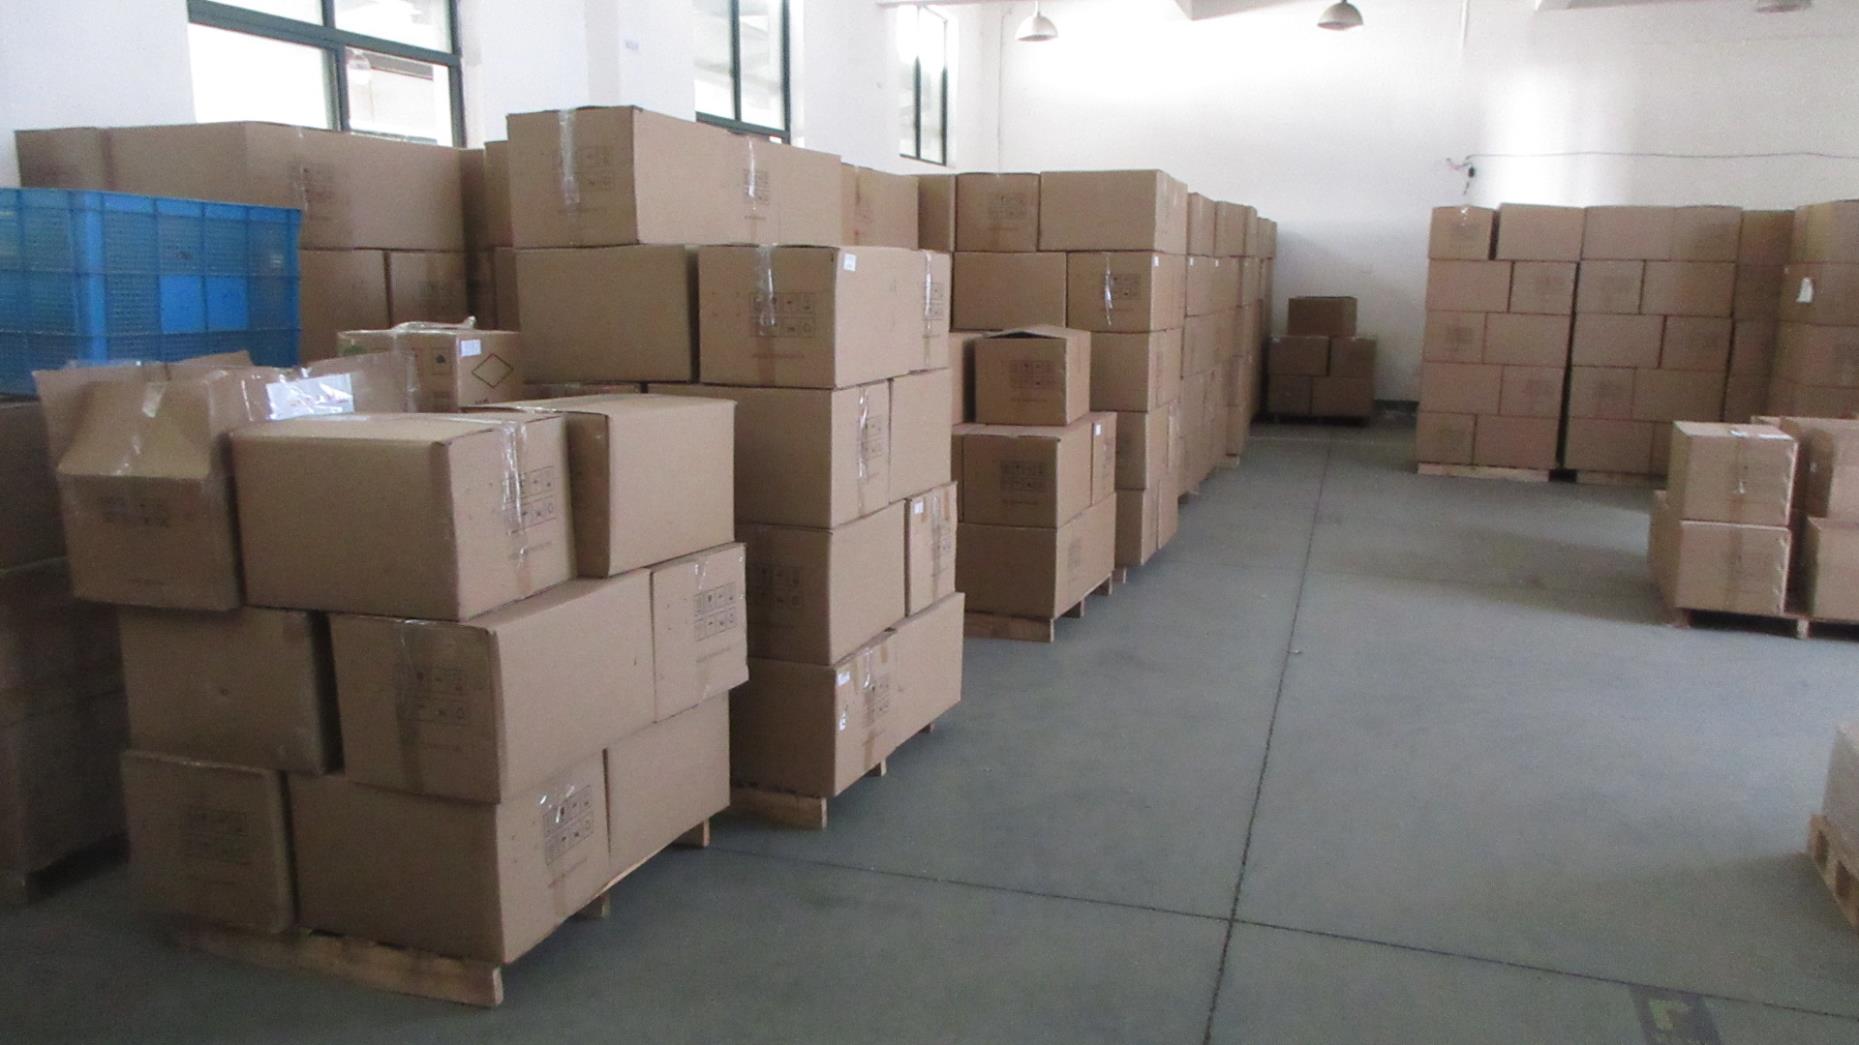
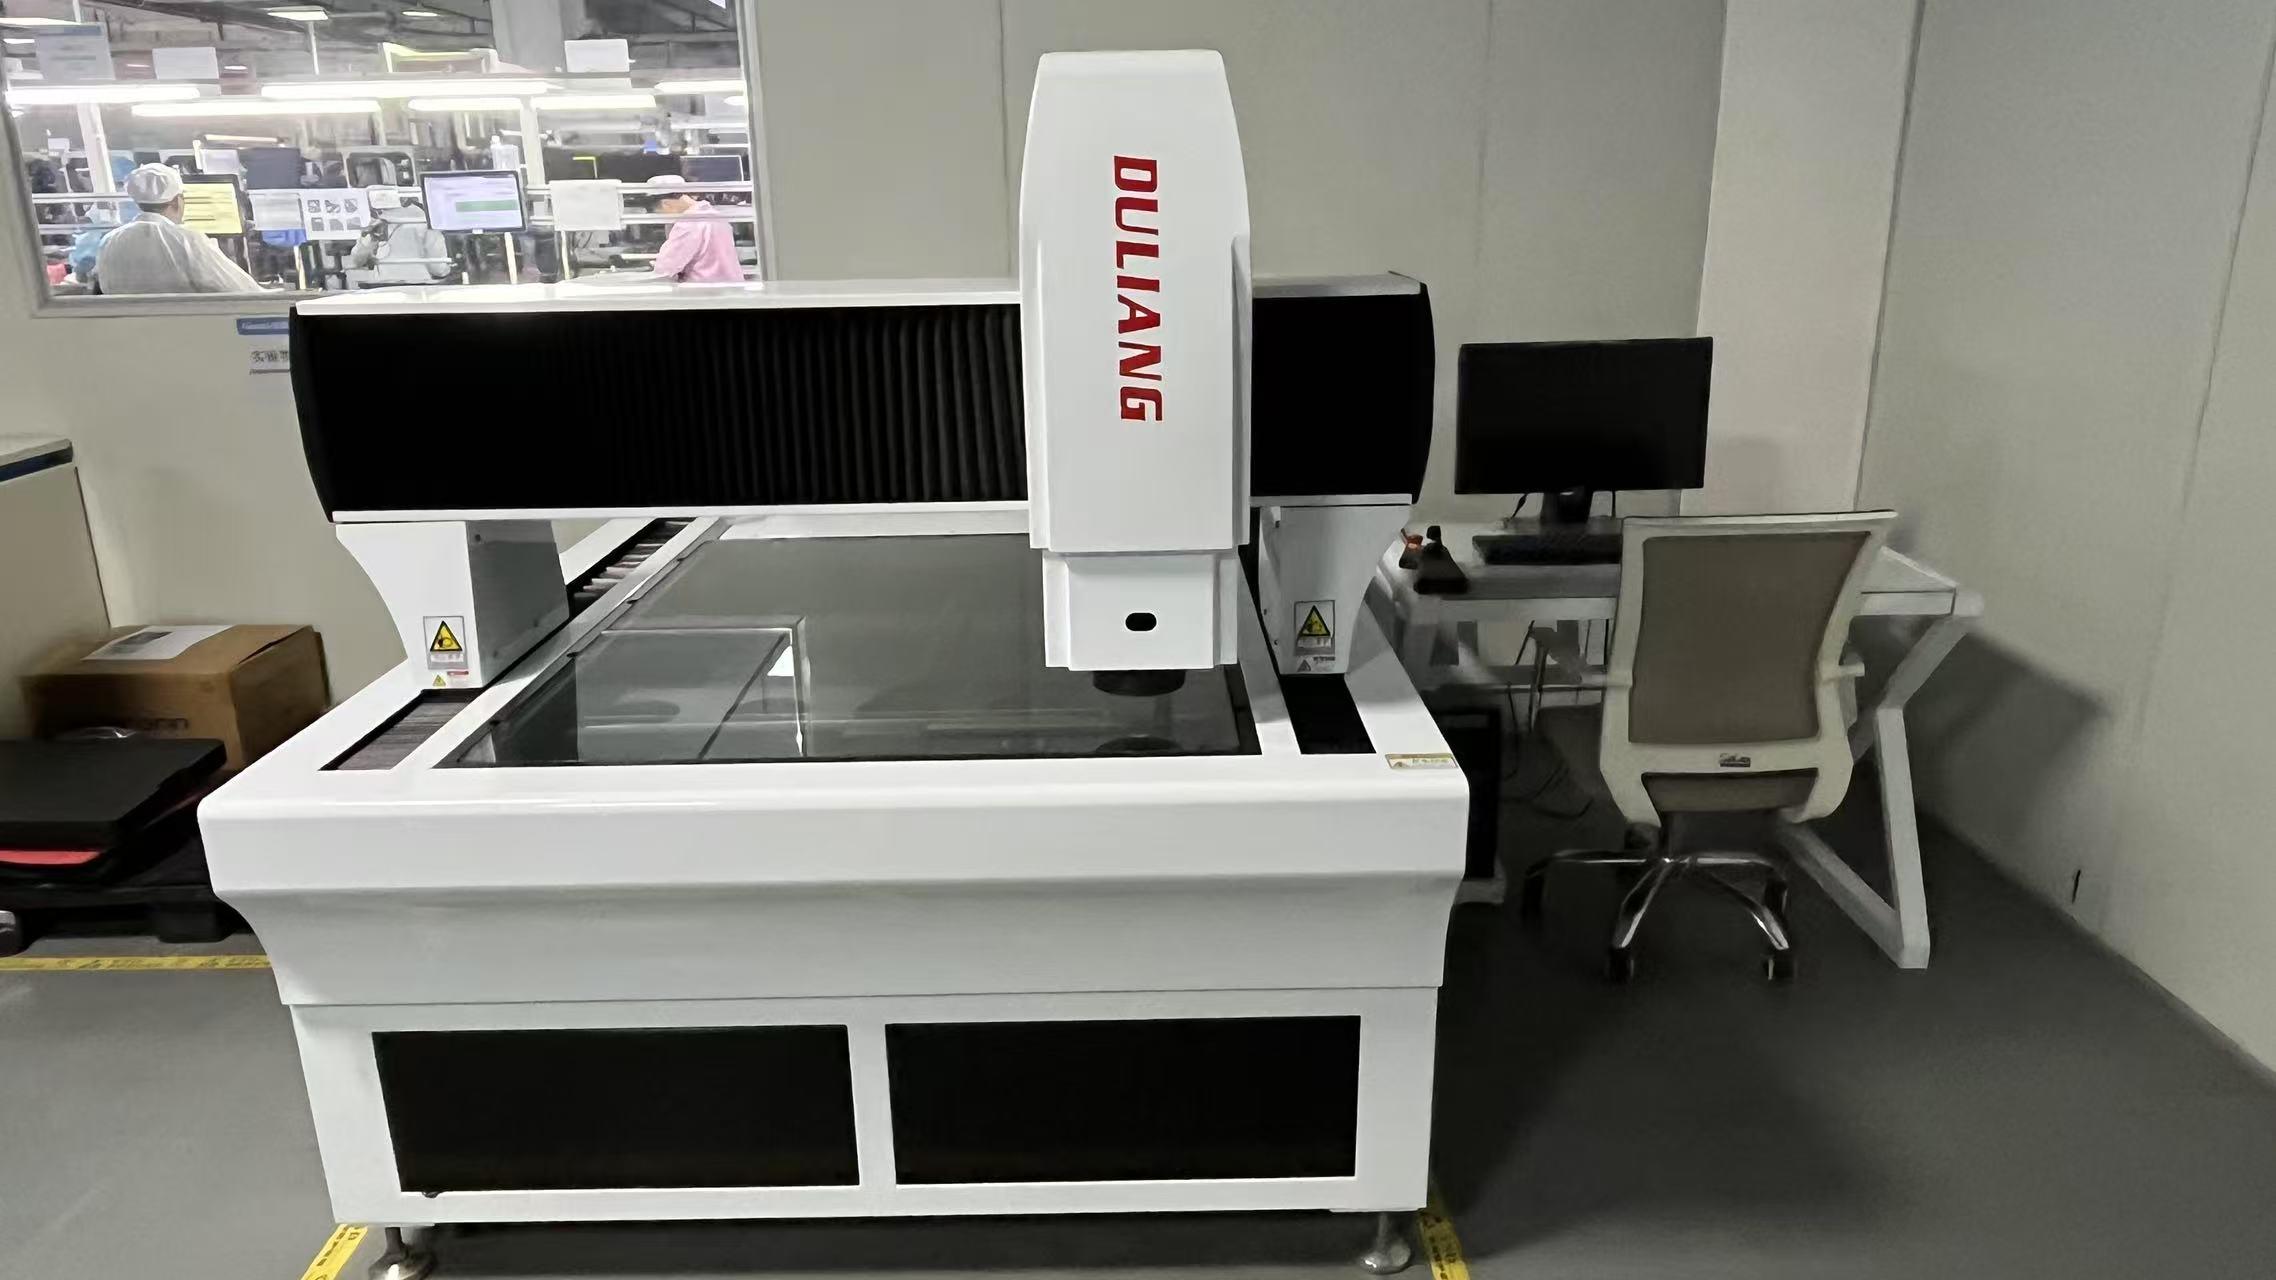
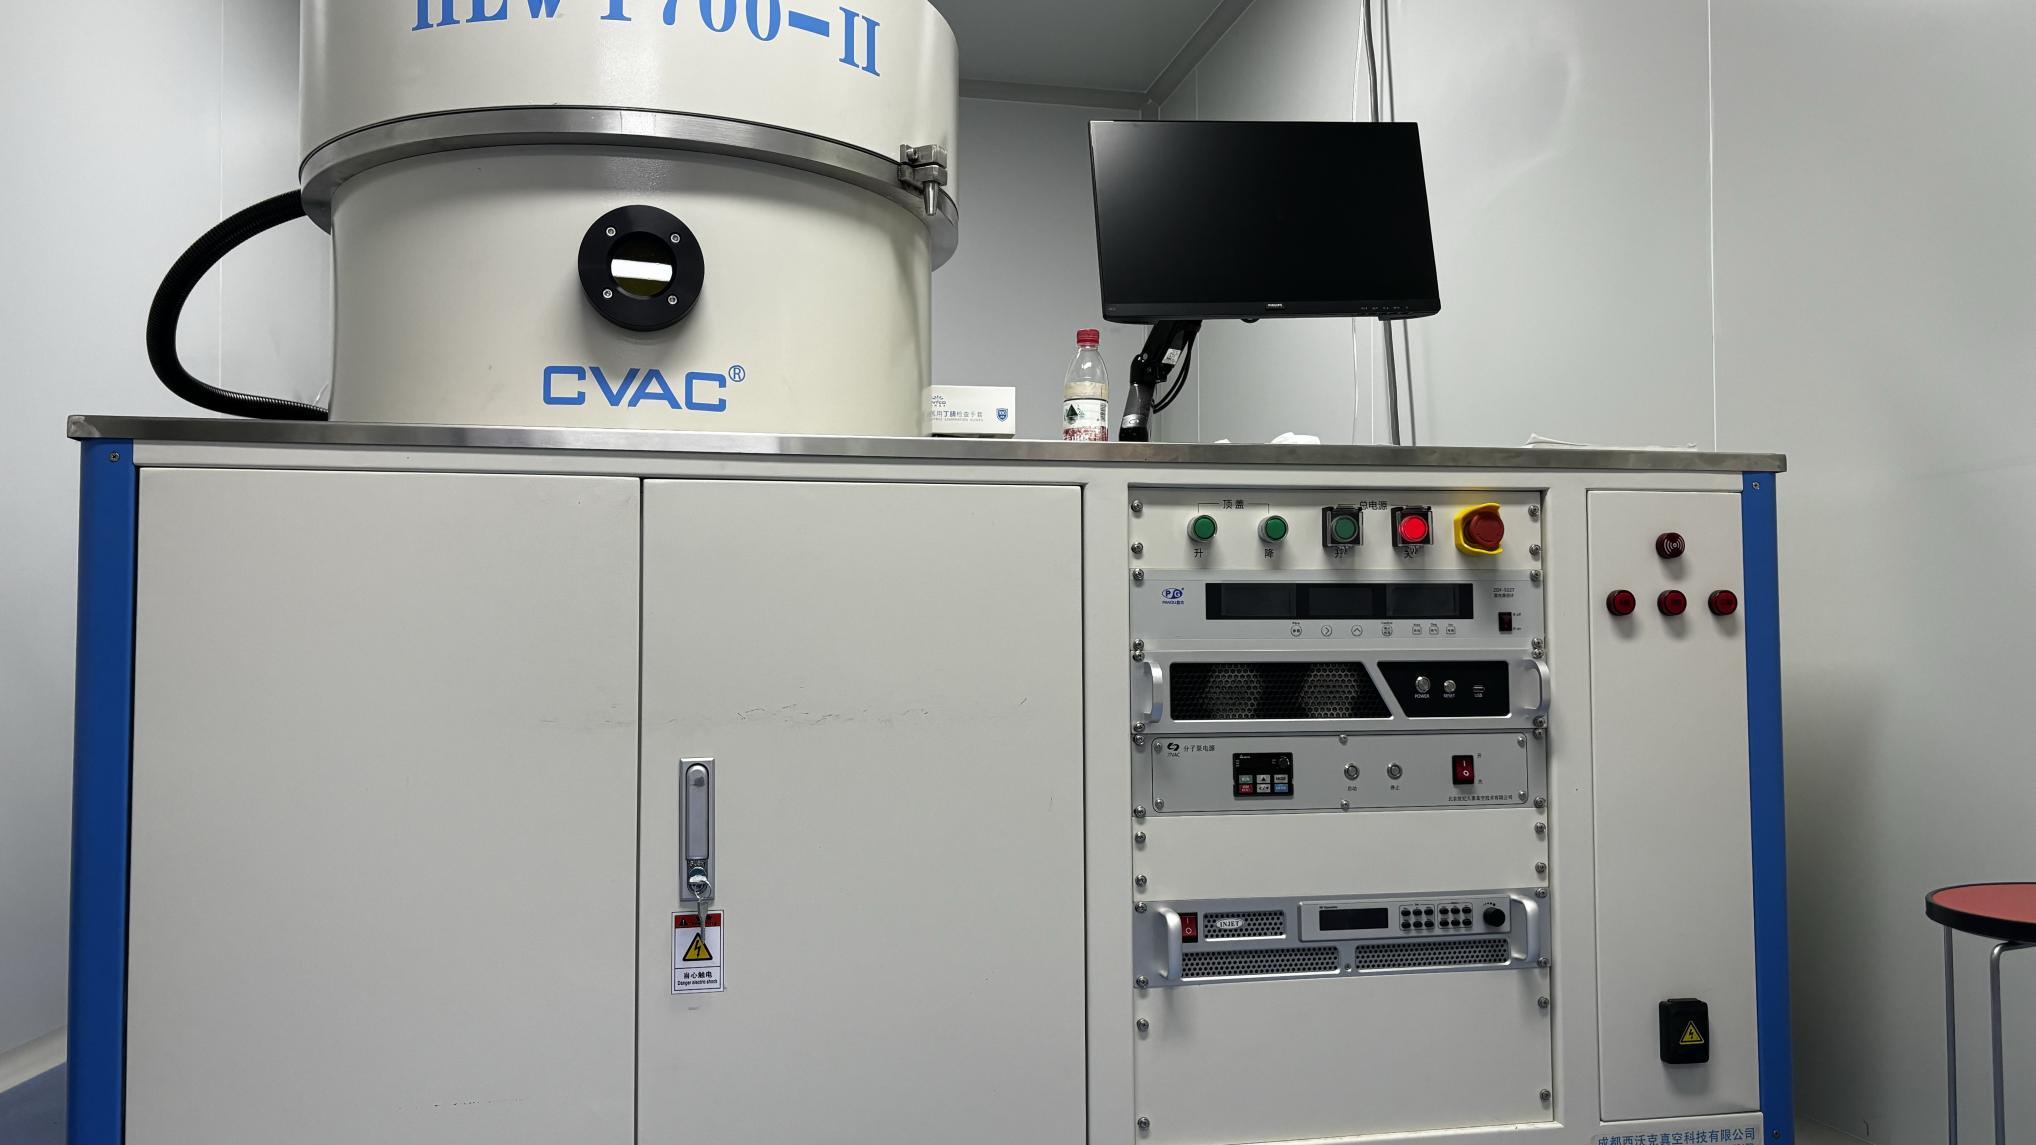
We simplify custom optical and electronic development for Geneva engineering firms. Our execution model from concept validation to large-scale production ensures compliance and cost stability.
Identify pathogen targets, required flow rate or surface space, beam angle requirements, and power supply standards.
Validate heating coefficients and radiation uniformity virtually prior to physical fabrication. Ensures the target dosage (mJ/cm²) is hit efficiently.
Ship structural prototypes to your laboratory in Geneva for spectral validation, safety checks, and biological performance evaluation.
Begin full-scale production inside our quality-controlled factory. Handle custom customs clearing processes directly into the Geneva canton.
High-temperature resistant heatsinks, heavy-duty cooling modules, and industrial-grade memory hardware supporting IoT servers and processing units deployed in Geneva's cleanroom and water-treatment hubs.
 Memvora